CAS: 1318-02-1
Molecular Formula: Al₂O₅Si
Molecular Weight: 162.05
EINECS: 930-915-9
HS Code: 28421000
Synonyms: Molecular sieve; Aluminosilicate; Synthetic zeolite; Natural zeolite; Zeolum
 EN
Mikem offers high-performance, superior quality, and reliable products to optimize your projects and achieve the best results.


CAS: 1318-02-1
Molecular Formula: Al₂O₅Si
Molecular Weight: 162.05
EINECS: 930-915-9
HS Code: 28421000
Synonyms: Molecular sieve; Aluminosilicate; Synthetic zeolite; Natural zeolite; Zeolum
Zeolite CAS 1318-02-1 is a porous crystalline aluminosilicate widely used as a molecular sieve, adsorbent, ion exchanger, and catalyst in industrial, environmental, water treatment, and detergent applications.
| Item | Value |
| Appearance | White powder |
| Melting Point | >1600 °C |
| Density | 1.9–2.3 g/cm³ |
| pH (H₂O) | 8–11 |
| pKa | 10.348 at 20 °C |
| Storage Condition | No special restrictions |
Mikem offers flexible packaging options, including 25 kg fiber drums for liquid products and 15–25 kg PP/PE bags for powder products, all customizable to meet your specific needs.
Mikem is ready to help you find the best solution.

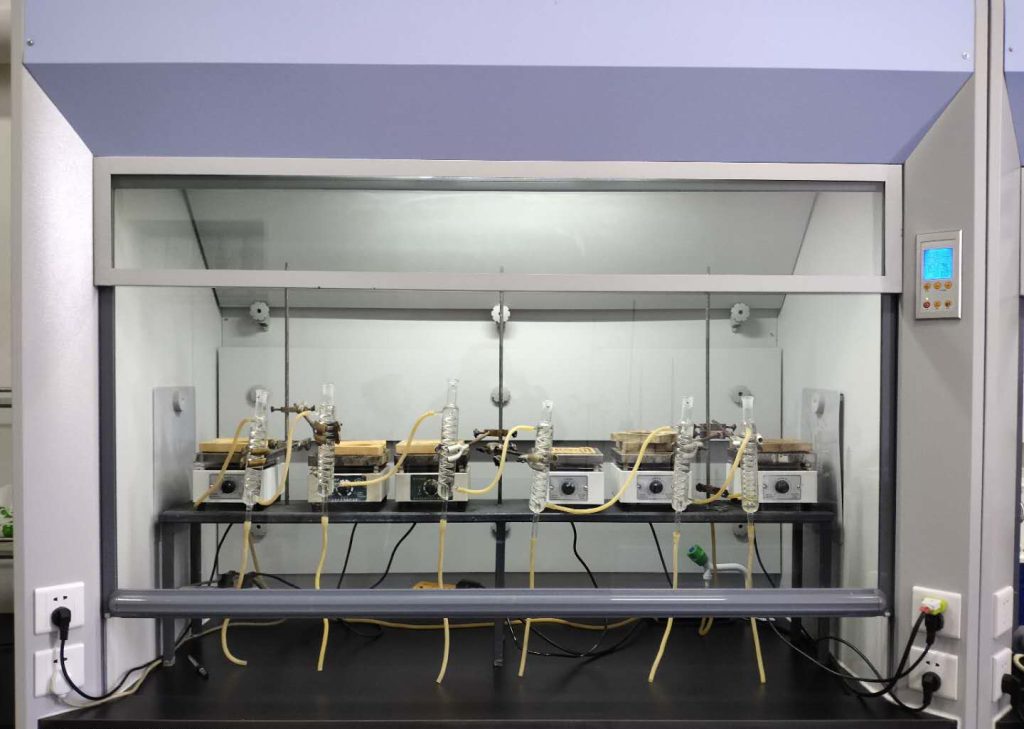
Our R&D laboratory, staffed by experienced chemists and engineers, drives continuous innovation— developing high-performance chemical solutions tailored to diverse industries. From raw material analysis to final product inspection, we maintain full traceability and consistency.
Founded in 2020, Mikem Chemical Group Co., Ltd. is a trusted global partner in the chemical supply chain, offering a wide range of inorganic and organic compounds, cleaning agents, pigments, additives, and APIs. With over 300 employees and a 20,000 m² facility integrating production, R&D, testing, and storage, Mikem delivers reliable products and tailored solutions that create lasting value for customers worldwide.

At Mikem Chemical Group, our commitment lies in providing dependable goods and customized approaches, fostering enduring benefits for clients across the globe.
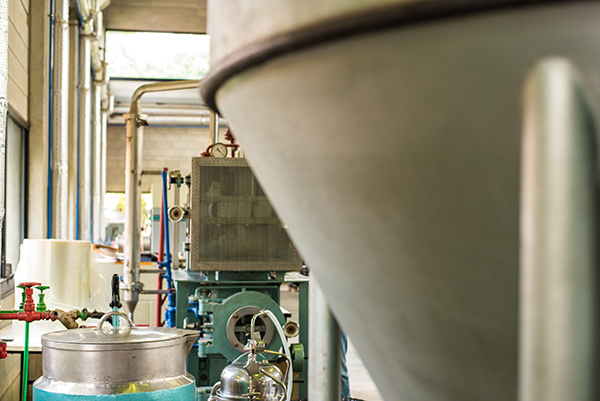

At Mikem, our advanced factory and laboratory form the foundation of our chemical production excellence. Equipped with modern manufacturing lines and precision testing instruments, we ensure every product meets strict international standards for quality, safety, and performance.
Our R&D laboratory, staffed by experienced chemists and engineers, drives continuous innovation— developing high-performance chemical solutions tailored to diverse industries. From raw material analysis to final product inspection, we maintain full traceability and consistency.